Advanced Supply Chain Management strategies involve using innovative planning, technology, and risk management practices to create supply chains that are resilient, adaptable, and aligned with business goals. An Advanced Supply Chain integrates data, technology, and smart analytics to make better decisions in the business. Right from predicting customer demand to cutting down costs and managing risks – every aspect is data-driven.
Advanced supply chain management (SCM) optimizes the flow of goods from raw materials to final delivery using Artificial Intelligence, Internet of Things, Blockchain, and Big Data Analytics to create resilient, data-driven, and agile operations. It moves beyond traditional logistics to incorporate strategic planning, “touchless” automation, and real-time visibility, enhancing operational efficiency and customer experience.
Key Components and Technologies
Artificial Intelligence (AI) & Machine Learning: Artificial Intelligence (AI) and Machine Learning (ML) revolutionize supply chain management (SCM) by automating processes, reducing costs, and boosting resilience against market disruptions. They replace reactive, manual planning with predictive, data-driven ecosystems. Key applications of AI & Machine Learning in Advanced SCM are below:
- Demand Forecasting: ML models (such as neural networks) analyse historical sales, seasonality, and external data to predict customer demand with high accuracy, minimizing both stock outs and overstocking.
- Logistics & Route Optimization: AI evaluates live traffic, weather, and fuel data to dynamically reroute shipments, mimicking a “live GPS” for cargo.
- Inventory Management: Automated tracking and replenishment systems adjust stock levels dynamically based on lead times and market fluctuations.
- Risk & Disruption Management: Generative AI and predictive modelling help identify geopolitical, economic, or environmental vulnerabilities, allowing companies to quickly source alternative suppliers.
Internet of Things (IoT): IoT in advanced Supply Chain Management (SCM) involves embedding connected sensors and RFID tags into physical assets to create a continuous, real-time data stream. It transforms static supply chains into agile, autonomous networks by automating inventory tracking, enabling predictive maintenance, and ensuring end-to-end operational visibility. Here are the few core use cases of using IoT in advanced SCM:
- Real-Time Asset Tracking: GPS and RFID trackers provide exact location, status, and environmental conditions (e.g., temperature, humidity) of goods in transit.
- Cold Chain Monitoring: Essential for the pharmaceutical and food industries, IoT continuously monitors temperature-sensitive products, triggering automated alerts if goods are compromised.
- Predictive Maintenance: IoT sensors on manufacturing machinery and transport fleets monitor vibrations and wear, identifying potential breakdowns before they occur to eliminate costly downtime.
- Automated Warehousing & Inventory: Smart shelves and automated guided vehicles (AGVs) provide up-to-the-minute stock visibility, optimizing picking and reducing fulfilment errors.
- Risk Mitigation & Contingency Planning: Real-time data streams factor in external variables like weather and traffic, enabling managers to dynamically re-route shipments and avoid bottlenecks.
Block Chain: Block Chain in advanced supply chain management (SCM) provides an immutable, decentralized ledger that links stakeholders. It eliminates data silos and paper trails to guarantee the authenticity of goods, automate vendor payments, and accelerate cross-border logistics through a single source of truth. Here are the key applications of Block Chain in advanced SCM:
- Provenance & Traceability: Tracks products from raw material origin to final consumer. This is critical for ethical sourcing, verifying organic/fair-trade labels, and stopping counterfeit products.
- Smart Contracts: Automates manual, error-prone administrative tasks. These self-executing contracts release payments automatically once predefined delivery or quality conditions (e.g., IoT temperature sensors validating a cold chain) are met.
- Fraud & Error Reduction: Eliminates reliance on single third-party intermediaries and prevents conflicting data across ERPs. Tamper-proof logs ensure that no single partner can retroactively alter transaction or shipment details.
- Recall Management: Drastically reduces the scope and time of recalls by allowing companies to trace defective components to the exact batch and supplier in seconds.
Advanced Planning and Scheduling (APS) Systems: Advanced Planning and Scheduling (APS) systems are intelligent software solutions that optimize supply chain operations by synchronizing materials, labour, and machine capacity. Unlike traditional systems, APS uses finite capacity scheduling and real-time algorithms to dynamically balance supply with demand while minimizing costs and lead times. Here are how APS is transforming supply chains:
- Finite Capacity Scheduling: Unlike legacy ERP systems that often assume infinite resources, APS schedules tasks based on exact machine availability, labour skill sets, and maintenance schedules to prevent bottlenecks.
- Real-Time Material Synchronicity: Integrates with your procurement modules to align raw material delivery with production start dates, supporting Just-In-Time (JIT) manufacturing and reducing inventory carrying costs.
- Fraud & Error Reduction: Eliminates reliance on single third-party intermediaries and prevents conflicting data across ERPs. Tamper-proof logs ensure that no single partner can retroactively alter transaction or shipment details.
- “What-If” Scenario Modelling: Enables planners to simulate supply disruptions, rush orders, or capacity changes to evaluate the best course of action before committing to a schedule.
- Capable-to-Promise (CTP): Provides highly accurate delivery dates to customers during the order-entry phase by checking real-time material and machine capacity.
- Dynamic Sequencing: Automatically sequences production runs to minimize machine setup times, changeover waste, and tooling adjustments.
Big Data Analytics: Big data analytics transforms supply chain management by processing vast amounts of structured and unstructured data (from IoT sensors, GPS, and POS systems) to enable proactive, data-driven decision-making. It shifts operations from reactive to prescriptive, reducing inventory holding costs, optimizing logistics, and mitigating risks. Here are the key benefits of Big Data Analytics in Advanced SCM:
- Demand Forecasting: Analyses historical sales, market trends, social media, and weather data to predict consumer demand accurately. Organizations utilizing big data for forecasting can see up to a 20% reduction in inventory holding costs and significant improvements in forecast accuracy.
- Logistics & Route Optimization: Integrates real-time traffic data, GPS tracking, and weather forecasts to dynamically route fleets. This minimizes fuel consumption, reduces transportation costs, and ensures timely deliveries.
- Supply Chain Risk Management: Uses predictive analytics to monitor geopolitical events, natural disasters, and supplier vulnerabilities. This allows companies to map procurement dependencies and activate contingency plans before disruptions impact the bottom line.
- Predictive Maintenance: Relies on IoT sensors attached to machinery and transport vehicles to monitor performance data in real time. Analytics can identify anomalies before a breakdown occurs, preventing costly manufacturing downtime.
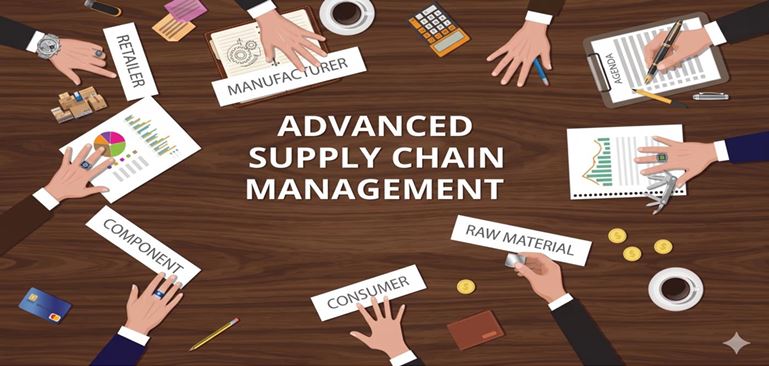
Core Strategies for Advanced SCM
- End-to-End Visibility: End-to-End Visibility means having complete, real-time transparency from raw material sourcing to final customer delivery. In advanced supply chain management (SCM), core strategies link physical, financial, and informational flows to shift operations from a reactive state to proactive, data-driven orchestration.
- Risk Management & Resilience: Supply Chain Risk Management (SCRM) and resilience are critical board-level priorities. Organizations utilize these frameworks to identify, assess, and mitigate threats while building systems that can absorb shocks and adapt to dynamic market conditions without halting operations.
- Customer-Centricity: Customer-centricity in advanced Supply Chain Management (SCM) shifts the traditional operational focus from cost reduction and internal efficiency to delivering hyper-personalized, frictionless, and responsive end-to-end consumer experiences. It treats the entire supply chain as a value-creation tool rather than just a logistical expense. .
- Continuous Improvement: Continuous improvement (CI) in advanced Supply Chain Management (SCM) focuses on making iterative, data-driven refinements to core strategies— planning, sourcing, making, and delivering. By systematically eliminating inefficiencies, CI turns supply chains from reactive operations into resilient, cost-efficient, and customer-centric networks.